

Home / Blog / Industry News / How Custom Packaging Supports Private Label Home Fragrance Product Development
How Custom Packaging Supports Private Label Home Fragrance Product Development
Content
Custom packaging fixes four physical variables before a single fragrance is approved: fill volume, headspace, impact tolerance and shelf footprint. Change any one of them after tooling is cut, and the project absorbs a new die, a new insert and a full re-run of transit testing.
In private label home fragrance, custom packaging is the engineered set of primary container, closure or insert, folding carton and outer shipper that is specified, drop-tested and printed to a brand's own dimensions and artwork, and sold under that brand's label rather than the manufacturer's.
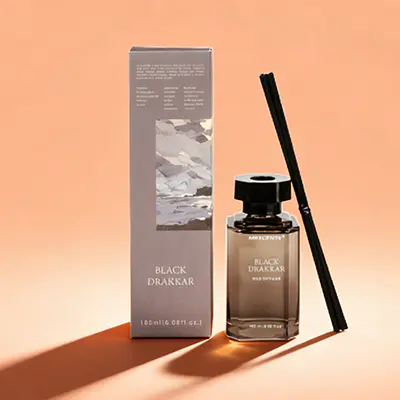
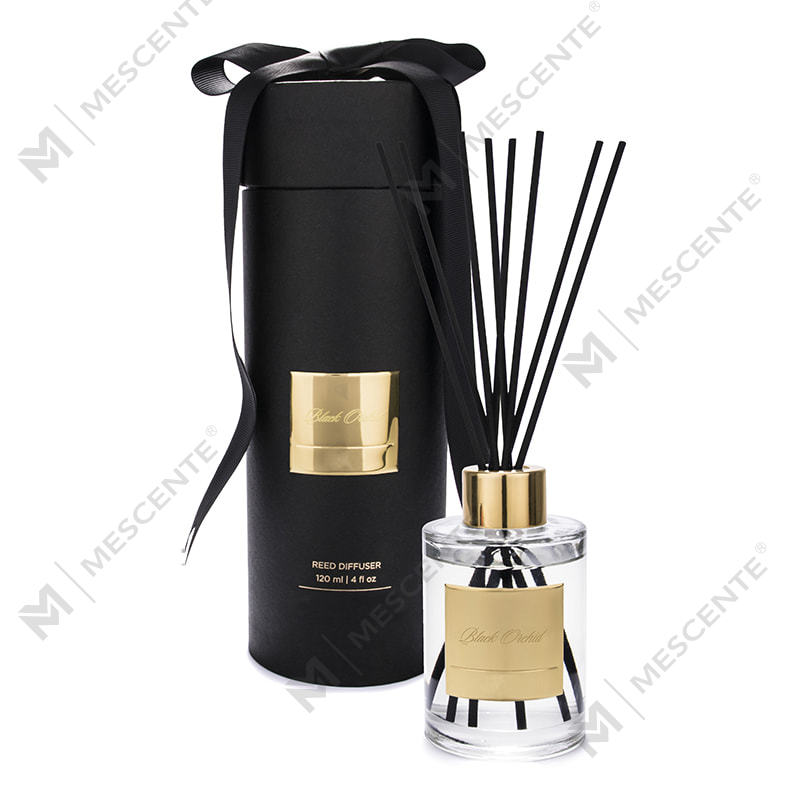
The result is that packaging decisions reach back into manufacturing. A 180 ml reed diffuser with a 24 mm neck accepts one family of caps and one insert geometry; the same body with a 30 mm neck accepts another. Vessel and closure are chosen together, and the carton, insert and pallet pattern follow from that pair.
None of these items is an artwork task. All four are engineering decisions with a written specification attached, and each one is far cheaper to change on paper than on a purchase order.
Four layers need sign-off before any tooling is cut: primary container, closure or insert, folding carton and outer shipper. Each layer owns a separate specification, and skipping one pushes a dimensional problem downstream into production.
| Packaging layer | What it controls | Specification to agree |
| Primary container | Fill volume, unit weight, fragrance contact | Glass or ceramic vessel, 180 to 220 ml nominal, neck finish matched to the closure |
| Closure and insert | Leak path and movement in transit | Screw cap with agreed torque, moulded pulp or EVA insert, 2 to 3 mm clearance |
| Folding carton | Shelf presence and regulatory panel | 350 to 400 gsm folding boxboard, matte lamination, four colour plus one spot |
| Outer shipper | Pallet efficiency and drop performance | Single wall corrugated, 32 ECT grade, ISTA 1A report on file |
The table is deliberately ordered by cost of change. Moving a vessel wall or neck finish invalidates the closure, insert, carton and pallet pattern; moving the shipper grade invalidates only the transit test.
A 2 mm change in vessel diameter can retire an entire carton die, insert mould and pallet pattern. Freeze the vessel drawing first, then draw everything else around it.
ISTA 1A sets drop height by packed weight, and the top band is aggressive: any shipping unit up to 9.1 kg is dropped from 762 mm, while a unit between 45.4 kg and 68 kg is dropped from 305 mm. A master carton of twelve 180 ml glass diffusers weighs roughly 7 kg, so it sits in the hardest band.
This is why a fragrance brand cannot specify packaging by feel. A 350 to 400 gsm folding boxboard carton protects a candle on a retail shelf; it does not protect twelve candles in a parcel network. The insert, the corrugated grade and the carton dimensions have to be designed as one system, and then tested as one system.
Run packaging development in five stages, each closing with a signed document, and the launch date stops depending on luck. The sequence matters more than the calendar: a white sample approved before artwork saves a printed re-run, and a transit test completed before production release saves a recall.
Format and vessel brief
Decide format, nominal volume, vessel family and neck finish. The output is a dimensioned drawing with tolerances, not a mood board.
Structural white sample
Cut the carton and insert in plain board, load it with filled product, and check clearance, lid closure and pallet pattern before any colour is discussed.
Print proof and barcode verification
Approve colour against a physical proof, verify the EAN-13 or UPC-A symbol at 80 percent magnification or above, and lock the regulatory panel.
Transit test
Run ISTA 1A for a single parcel or ASTM D4169 for a distribution cycle, using filled and sealed product rather than empty containers.
Golden sample and specification release
Sign one physical reference unit and freeze the sheet, including board grade, print colours, adhesive and insert material.
Each stage produces a document a factory can build against. That is the difference between a packaging project and a series of opinions.
In the EU, CLP Regulation (EC) No 1272/2008 requires hazard pictograms and allergen declarations on the label, and in the United States, 16 CFR Part 500 sets the net quantity statement format. Both panels have to be reserved on the carton before the artwork is signed off, not squeezed in afterwards.
Practical items to freeze at proof stage:
There are two defensible allocations: a custom vessel with a stock carton, or a stock vessel with a custom carton and insert. The first buys shelf uniqueness and a proprietary silhouette; the second buys speed, lower minimum order quantities and cheaper reorders.
Most first-time private label launches sit in the second column, then migrate to the first once a scent has proven repeat purchase. That sequence keeps cash in marketing rather than in tooling, and it keeps the packaging brief reversible until the brand has real sell-through data.
Ask for six things in writing, and the packaging side of a private label project becomes auditable rather than conversational.
Manufacturers that already ship internationally tend to document their packaging rules rather than improvise them. Suzhou M-Scent Arts and Crafts Co., Ltd. covers packaging standards for international shipping of bulk scented candles alongside its private label candle and diffuser ranges, which is the kind of written reference a brand can attach to its own specification sheet.
At the format stage, before fragrance selection is finalised. Four specifications, namely fill volume, headspace, insert geometry and shipper grade, drive the filling line, the freight cost and the drop test, and each one costs more to change after tooling than before.
Usually, and mostly through tooling rather than materials. A stock vessel with a custom carton and insert can launch at a far lower quantity than a custom moulded ceramic vessel, because the investment sits in print plates and dies rather than in a mould.
ISTA 1A for single parcel shipments and ISTA 3A for parcel delivery environments; ASTM D4169 when the brand needs a full distribution cycle. Whichever is chosen, test filled and sealed product, never empty containers.
Three: a white structural sample, a printed proof and a golden sample. Three approvals catch the failures that matter, which are dimensional clearance, colour drift and insert compression.
Freeze four documents before the first production run: the vessel drawing, the carton die line, the approved artwork file and the transit test report.
Custom packaging is the cheapest part of a home fragrance launch to get right and the most expensive to get wrong. Specifying the four layers, testing the shipping unit at the correct ISTA 1A drop height and freezing artwork data early turns packaging from a launch risk into an asset the brand owns outright.
Address:
Building 10, No. 39, Muxu East Road, Mudu Town, Wuzhong District, Suzhou City, Jiangsu Province, China
Company
Products
Mobile
